
Key Takeaways
- Check the measurement before condemning the filters. A cartridge dust collector can display misleading differential pressure (DP) because of a blocked tap, leaking tube, reversed connection, or misconfigured instrument.
- A believable number may still be wrong. Compare pressure trends with actual airflow, fan operation, dust loading, and the independent symptoms covered in the cartridge dust collector maintenance guide.
- Low DP does not automatically mean healthy cartridges. Reduced airflow or dust bypass may also explain the reading. See the separate guidance on filter cartridge cleaning versus replacement.
- Automatic cleaning depends on trustworthy DP. If the sensor is wrong, clean-on-demand pulse control can start unnecessarily, stop too early, or fail to respond to actual loading.
- Verify the entire signal chain. Pressure tap, impulse tubing, gauge or transmitter, analog signal, controller scaling, and trend history all contribute to the final displayed value.
What Is Differential Pressure Actually Measuring?
Cartridge collectors typically measure pressure at the dirty-air and clean-air compartments. The difference indicates filter-section resistance when taps are correctly located. Dust loading generally raises resistance; effective pulse cleaning can lower it.
The definition matters because a fan can create substantial negative pressure in both compartments while the difference across the cartridges is relatively modest. For example, suppose the dirty side is at −800 Pa and the clean side at −1,100 Pa relative to ambient. The filter differential is 300 Pa, approximately 1.2 inches of water gauge. Neither −800 Pa nor −1,100 Pa by itself is the cartridge pressure drop.
DP also depends on airflow. Low DP at reduced fan speed may indicate less air through the media, not cleaner filters. A sudden DP fall with rising outlet dust may indicate damaged media or seals. Compare readings at similar operating conditions.
Follow the Measurement Chain, Not Just the Display
Dirty-Side and Clean-Side Pressure Taps
The dirty-side pressure connection is exposed to particulate and is especially susceptible to plugging. Fine powder, moisture, or sticky deposits can partly seal the opening. An obstructed tap may trap an old pressure signal or respond very slowly to changes. Depending on which side is blocked and the current fan conditions, the indicated DP may be too high, too low, frozen, or delayed; a blockage does not produce one predictable error direction.
A tap near an inlet jet, damper, or turbulent transition may not represent compartment static pressure. Confirm locations against drawings before recalibration.
Tubing, Condensate, and Incorrect Connections
Sensing tubes can crack, kink, detach, accumulate water, or deteriorate with heat and sunlight. Leaking fittings and condensate pockets can distort readings, making a healthy transmitter appear defective.
High and low connections must match the instrument’s configuration. On a typical negative-pressure collector, the dirty-side line goes to the specified high-pressure port and the clean-side line to the low-pressure port, because the dirty side is less negative. Reversed lines may produce negative, zero, or invalid indications, depending on the device. Follow the actual OEM wiring and port diagram rather than swapping tubing experimentally during operation.
Gauges, Transmitters, and Controllers
Mechanical gauges can lose zero or become damaged. Electronic transmitters introduce additional checks: power supply, sensor range, zero and span calibration, electrical wiring, analog output, and PLC or cleaning-controller scaling. A 4–20 mA transmitter configured for 0–10 in. w.g., for example, should nominally output 12 mA at 5 in. w.g. A controller configured for another span can show the wrong DP even if the transmitter is measuring correctly.
After transmitter replacement, check configuration before assuming a process upset; retain original settings.
Recognize the Most Common False-Reading Patterns
| Observed DP behavior | Possible measurement fault | First independent check |
|---|---|---|
| Near zero while airflow and dust loading continue | Reversed lines, disconnected tube, failed sensor, or actual media bypass | Confirm port connections and inspect emissions |
| Unchanging value through several cleaning cycles | Blocked tap, trapped signal, frozen instrument, or data-logging fault | Compare with a suitable reference instrument |
| Sudden high reading without matching airflow deterioration | Plugged sensing path, condensate, zero/span error, or real process change | Verify pressure lines and process conditions |
| Negative or out-of-range DP | Incorrect port assignment or electrical scaling | Check approved schematic and controller setup |
| Display and PLC history disagree | 4–20 mA wiring, scaling, or communications issue | Compare local indication, raw signal, and trend |
These are diagnostic clues, not proof. Confirm instrument and process readings before changing cleaning settings or replacing cartridges.
Differentiate a Real Filter Problem from an Instrument Problem
Compare DP with Actual Extraction Performance
Check pickup suction, fan speed, dampers, and outlet dust. DP should respond plausibly to substantial airflow and cleaning changes. If readings contradict other observations, verify the instrument first.
Where needed, measure airflow and static pressure with suitable calibrated instruments. Motor current is not an airflow measurement; compare results with the installed fan curve and baseline.
Evaluate Pulse Cleaning Recovery
A functioning clean-on-demand controller may pulse when DP reaches a high setpoint and pause after it falls to a lower setpoint. If a blocked sensing line reports a frozen high number, the system could continue cleaning even after the cartridges have recovered. A frozen low number could suppress needed cleaning. Either fault can disguise the actual condition of the cartridges.
Verify transmitter response before adjusting pulse settings. Then check compressed air, valves, hopper discharge, and DP at actual airflow; use the collector’s approved limits.
Check for Real Bypass or Low Airflow
Near-zero DP may reflect missing or torn filters, failed gaskets, or very low airflow. Rising outlet dust requires prompt bypass investigation, not praise for apparent cleaning.
A Safe Verification Procedure for Maintenance Teams
Work on pressure instruments should be performed by trained personnel following the collector and instrument manufacturers’ instructions. Isolate electrical, mechanical, and pneumatic energy as required, account for hazardous or combustible dust, and avoid creating an airborne dust cloud during cleaning. Never blow shop air into a connected transmitter or into an operating dust system without an approved procedure.
- Record the symptom. Note displayed DP, process load, fan speed, active branches, pulse-controller state, and any alarms or visible dust release.
- Verify installation details. Compare dirty/clean tap locations and high/low tubing connections with the approved drawings.
- Inspect the sensing path. Under safe isolation, look for blocked taps, dust-filled tubing, moisture pockets, cracked hose, loose fittings, or heat damage.
- Use a reference instrument. A qualified technician should compare both pressure points with a suitable calibrated manometer or DP reference, following the approved connection method.
- Check electrical scaling. For electronic systems, verify sensor span, zero, signal output, PLC scaling, alarm configuration, and any controller filter or damping settings.
- Restore and validate. Repeat readings under representative flow and observe whether pressure changes sensibly during a permitted cleaning cycle; document the findings.
Before comparing gauges, match reference points, ranges, zero references, and operating conditions.
What Published Industrial Cases Teach Us
The following are third-party documented cases, not Omela installations. Most involve fabric baghouses rather than cartridge collectors; the transferable lesson is the differential-pressure measurement chain, not an assumed identical filter or operating setpoint.
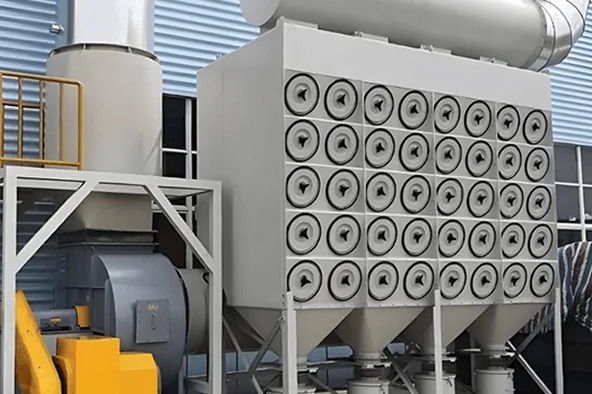
Gypsum Processing: Unreliable Instruments and Unnecessary Pulsing
In a published inspection of a gypsum-products facility in Bridgeport, Alabama, investigators described multiple unreliable differential-pressure readings associated with gauges and sensing lines in poor condition. Several collectors were also left operating in fixed timer mode, pulsing even when production was stopped. The inspection identified compressed-air moisture concerns as another system-wide maintenance issue.
No quantified filter-life improvement was reported. The lesson: validate gauges, sensing lines, and control logic before using DP trends to justify cleaning or filter changes.
Dryer-Mixer Baghouse: Pressure Was Not Measured Across the Filters
At another publicly documented gypsum facility in Fort Dodge, Iowa, repeated filter failures led to extensive maintenance spending. The field assessment identified several process and equipment problems, including a fundamental instrumentation error: differential pressure was not being measured across the baghouse itself. Other findings concerned drying conditions, duct geometry, missing pre-separation, and collector configuration.
The recommendation included true filter DP monitoring and process checks. It did not establish that correcting DP alone solved failures. Even a calibrated gauge cannot report filter resistance when connected to the wrong locations.
Glass-Additive Manufacturing: A Broken Gauge Became a Compliance Failure
A U.S. Department of Justice account described a glass-additive manufacturer whose loadout baghouse had a broken DP gauge while operations continued. Employees submitted daily readings and reports that falsely indicated compliant monitoring. In June 2015, the company was sentenced to pay a $325,000 fine, along with probation and an environmental compliance plan, for Clean Air Act false-statement violations.
This was a baghouse regulatory case, not evidence of cartridge failure. The violation involved knowingly falsified records, not a broken gauge alone. Keep accurate monitoring records and follow permit reporting rules.
Design the Sensing System for Reliability
Good measurement begins with the installation. Pressure taps should sample representative compartment static pressure and remain accessible for approved maintenance. Tubing should be routed to reduce exposure to damage and minimize condensate accumulation, using materials compatible with the temperature and environment. For outdoor collectors, protect lines and instruments against weather and ultraviolet exposure.
Plants handling particularly dusty material may need maintainable taps, protective arrangements, or an engineered method of keeping impulse lines clear. Any purge arrangement must be designed so it does not distort measurements or introduce a hazard. Instrument selection should consider range, accuracy, required alarms, environmental protection, response time, and compatibility with the cleaning controller.
A dashboard or premium transmitter cannot compensate for blocked taps or incorrect scaling.
Maintain a Baseline and a Traceable Inspection Record
A trustworthy DP trend is most useful when it is linked to operating context. Record the reading at similar fan speed and production load, note cleaning activity, and investigate abrupt deviations. After replacing a sensor or cartridge set, establish a fresh baseline without discarding previous records.
| Monitoring record | Information to retain | Why it matters |
|---|---|---|
| Pressure reading | Local DP, controller DP, units, time | Reveals instrument disagreement |
| Process conditions | Fan speed, active branches, production load | Makes historical comparisons meaningful |
| Sensor inspection | Tap condition, tubing, calibration reference | Documents measurement reliability |
| Cleaning response | Pulse sequence, start/stop thresholds, DP recovery | Detects control or cleaning abnormalities |
| Corrective action | Repair, replacement, technician, retest | Prevents recurring unverified faults |
Where an air permit specifies monitoring frequency, acceptable range, testing, and reporting, those requirements take precedence over general maintenance advice. A sudden instrument failure should trigger the site’s designated reporting and repair procedure, not an estimated entry in the logbook.
Final Engineering Recommendation
An unexpected differential-pressure reading is a reason to investigate, not an automatic instruction to replace cartridges. First establish whether the sensor is measuring the intended dirty-to-clean pressure difference. Then verify the taps, lines, gauge or transmitter, controller scaling, actual airflow, and physical filter condition.
For technical support, provide collector model, tap positions, tubing photos, DP history, airflow conditions, controller settings, and symptoms. These records help distinguish instrument failure from real filter resistance or bypass.
FAQ
Can a Blocked Pressure Tap Cause a False High or Low Differential Pressure Reading?
Yes. A plugged tap can trap or delay the pressure signal. Depending on which side is blocked and how operating pressure changes, the display may read too high, too low, or remain nearly constant. Verify both taps and lines before drawing conclusions.
Why Does My Cartridge Dust Collector Show Zero Differential Pressure?
Possible causes include reversed or disconnected sensing lines, a failed gauge or transmitter, incorrect controller scaling, reduced airflow, or actual filter bypass. Check the measurement circuit and outlet dust condition; zero does not automatically mean the cartridges are clean.
How Can I Test a Dust Collector Differential Pressure Sensor?
A qualified technician should compare the installed reading with a calibrated reference instrument connected to the correct pressure points, using the manufacturer’s safe procedure. Electronic systems also require checks of zero, range, output signal, wiring, and controller scaling.
Can Incorrect DP Readings Affect Pulse-Jet Cleaning?
Yes. In a clean-on-demand system, the DP signal controls when cleaning starts and stops. A falsely high reading may cause unnecessary pulses; a falsely low or frozen reading may delay cleaning. Confirm sensor accuracy before changing cleaning thresholds.
How Often Should Differential Pressure Tubing and Gauges Be Inspected?
Follow the OEM manual, dust severity, operating environment, and any permit requirements. Inspect sooner when readings become unstable or implausible, after instrument work, or when dust and moisture commonly affect the sensing lines. Keep calibration and repair records.
Author
Jessica Ma – Senior Filtration Engineer, Omela Filtration
Jessica Ma is a senior filtration engineer at Omela Filtration, specializing in dust and liquid filtration. With over 15 years of experience, she focuses on optimizing baghouse performance, enhancing filtration efficiency, and developing high-performance solutions for industrial dust collectors and precision liquid filtration applications.